Optruss

Resonant High-Frequency Acoustic Emission & Ultrasound Sensor

The earliest warning system on the P-F curve: detecting sub-micron lubrication film degradation, microscopic metal-to-metal contact, and pressurized gas leaks at 38 kHz.

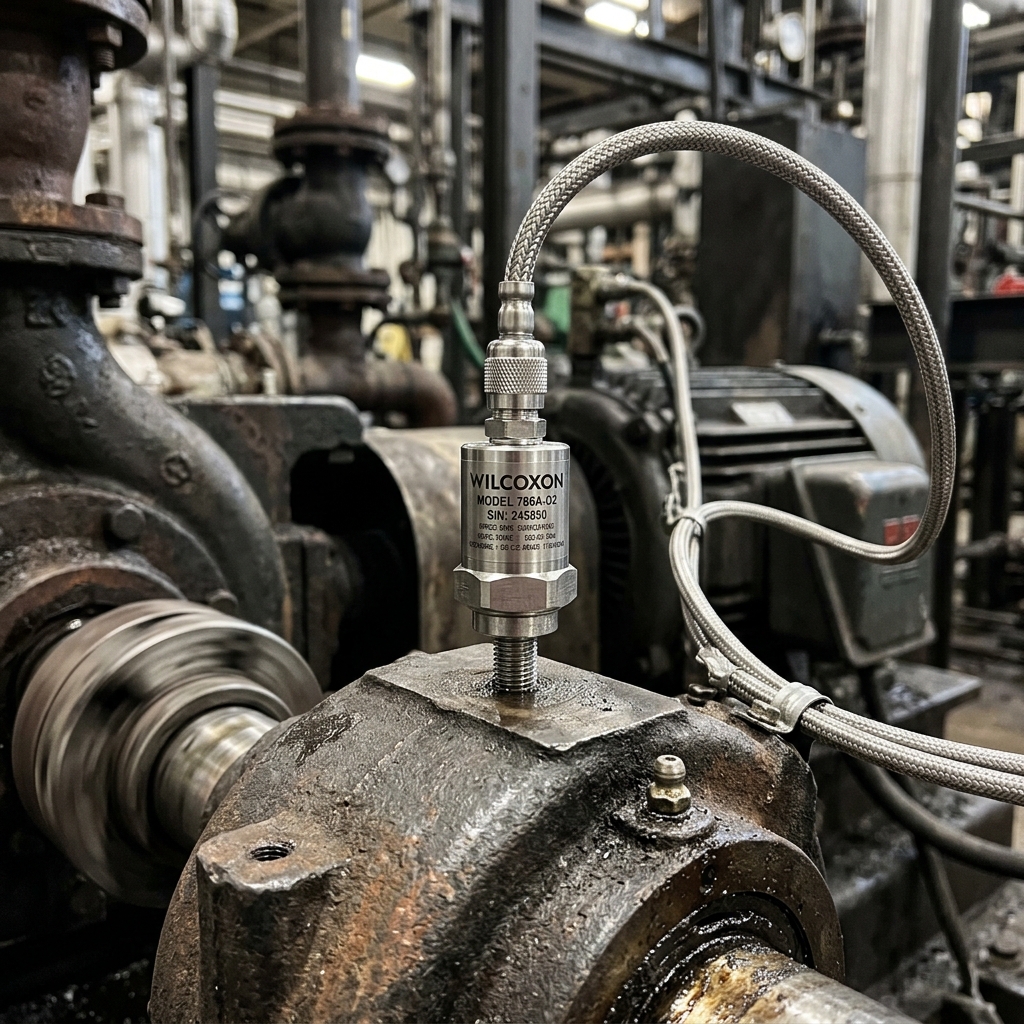
Wilcoxon 786A vibration sensor mounted on the bearing housing of a running pump

Stage 1: Microscopic Friction & Sub-Surface Shear

Provides the absolute earliest intervention point. When lubricating oil or grease film thins below hydrodynamic thickness, surface asperities make microscopic contact, generating 38 kHz stress emissions months before any temperature rise or standard vibration velocity change.

Operating Principle & Signal Chain

Physical Transduction Mechanism

Friction, turbulence, and structural impacts release high-frequency acoustic stress waves (> 20 kHz) that travel through machine structures before lower-frequency mechanical vibrations develop. The sensor employs a high-Q resonant piezoelectric ceramic disc tuned sharply to 38 kHz. An internal heterodyne circuit mixes this ultrasonic frequency with a local oscillator, translating ultrasonic stress signals into audible frequencies while computing RMS and peak dBµV.

Electronic Signal Chain Architecture

High-Q 38 kHz Piezo Crystal → High-Pass Preamp (fc = 20 kHz) → Balanced Heterodyne Mixer with Local Oscillator → 0-5 kHz Audio Low-Pass Filter → RMS Decibel Converter → 24-bit 200 kS/s Acoustic ADC → Optruss Acoustic Lubrication Engine.

Direct Acoustic Coupling to Bearing Housing Load Zone

  • Clean bearing housing surface to bare metal; remove thick flaking paint coats

  • Apply thin smear of high-viscosity acoustic coupling gel or synthetic grease

  • Ensure waveguide axis points directly toward the inner raceway contact zone

  • Verify baseline decibel reading under normal loaded running conditions

Wiring & Shield Grounding Specifications

Ultrasonic waves attenuate rapidly across air interfaces and joint boundaries. The sensor waveguide must be mounted directly onto the solid metal casing of the bearing load zone. For permanent installations, use 10-32 threaded stud with silicon acoustic couplant. For routine monitoring, use high-strength magnetic waveguide with rare-earth core.

Field Commissioning Checklist

Detectable Degradation Profiles

True RMS dBµV threshold elevation (> 8 dB above baseline)

Uniform high-amplitude white noise hiss across the 38 kHz band with drop back to baseline upon grease injection

Acoustic emission transient burst rate & energy count

Short-duration (10-50 µs) high-energy transient spikes breaking through quiet baseline during roller pass

Directional ultrasound parabolic amplification

Constant high-frequency turbulent hiss generated by sonic pressure drop across microscopic orifice

Acoustic cycling profile timing comparison

Continuous rushing sound without clean mechanical shut-off snap, indicating blow-through steam loss

Hardware-Accelerated Edge Acquisition & AI Classification

Optruss Acoustic Agent monitors live decibel trends and calculates Crest Factor. When an 8 dBµV elevation is sustained without corresponding speed or load changes, AssetCore generates an automated Condition-Based Lubrication Work Order specifying exact grease volume in grams, closing the loop before metal wear begins.

Optruss Edge Sovereign Industrial Hub (Air-Gapped)

Deterministic high-speed acquisition and local AI inference: running air-gapped on DIN rails with FPGA DSP, dual isolated Ethernet, and sovereign Merkle audit ledger.

Stream Resonant High-Frequency Acoustic Emission & Ultrasound Sensor Directly to Optruss Edge

Benefit from sub-millisecond edge FFT processing, early P-F curve anomaly detection, and automated CMMS work order generation.